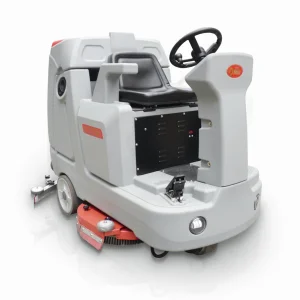
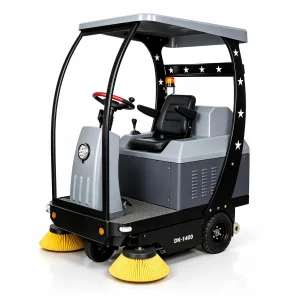
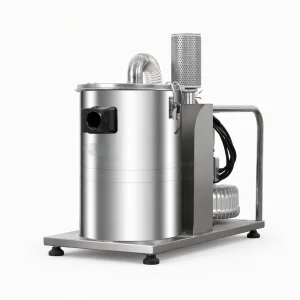
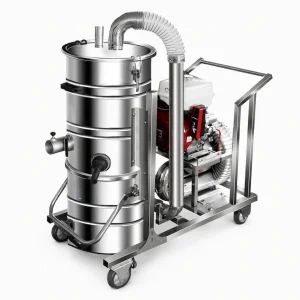
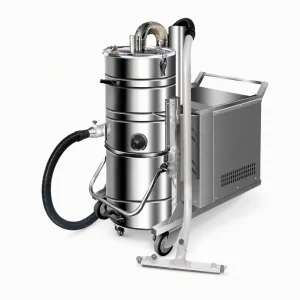
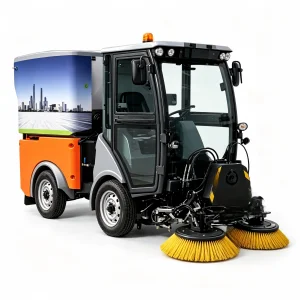
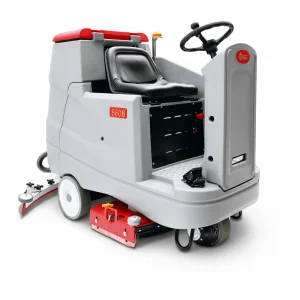
Industrial vacuum cleaners, sweepers, and ride-on floor scrubbers manufactured under rigorous CE and ISO9001 quality standards for restaurant kitchens, dining facilities, and food logistics centers.
The global market for commercial kitchen cleaning systems is experiencing a paradigm shift. Rising labor costs, aggressive public health regulations, and rapid turnaround requirements necessitate heavy-duty, factory-direct extraction machinery.
Hospitality networks globally face acute kitchen staffing shortages. Manual mopping and brushing fail to clear microscopic grease from textured quarry tiles, driving operators to deploy high-pressure continuous extraction vacuums to meet health code standards with 50% fewer labor hours.
Regulatory bodies such as the FDA, EFSA, and regional health inspectors have intensified auditing parameters regarding cross-contamination and air quality. Multi-stage wet-and-dry HEPA vacuums eliminate hazardous aerosolization of pathogens during washdowns.
Restaurant chains, central commissaries, and hospitality franchises are shifting away from fragmented consumer-grade equipment distributors. Direct partnerships with original equipment manufacturing (OEM) factories secure standard configurations, lowering total lifecycle maintenance costs.
Standard industrial vacuum systems fail prematurely in restaurant facilities due to high oil emulsion levels, moisture, and tight floor plans. DIKE factory engineers calibrate recovery equipment to specific physical zoning challenges.
Handles high-temperature fat splatter, cooking oils, and heavy grease pools around deep fryers. Requires oil-resistant NBR suction gaskets, fluoropolymer hydrophobic filters, and rapid-recovery wet vacuuming to eliminate catastrophic slip-and-fall hazards without corroding pump assemblies.
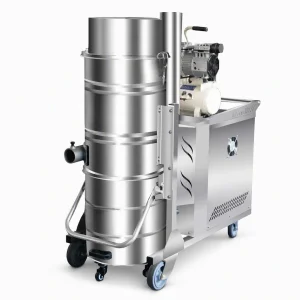
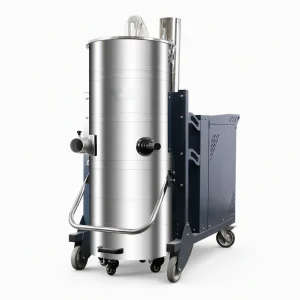
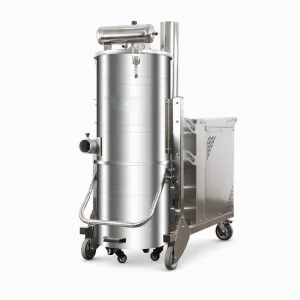
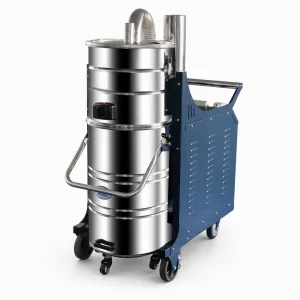
Environments containing airborne flour and starch carry combustible dust explosion risks (ATEX zones). Utilizes anti-static conductive hoses, stainless steel 304 tanks, and pulse reverse blow systems like the DK-221MFC to ensure micro-dust remains contained without filter blinding.
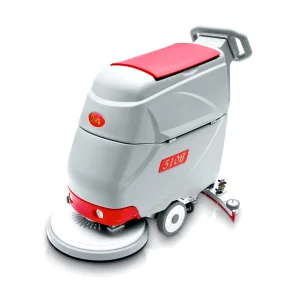
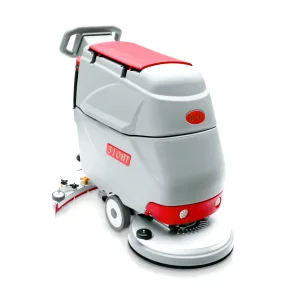
Customer-facing carpet and architectural stone flooring demand whisper-quiet decibel profiles (<62 dBA) during operational or transitional hours. Walk-behind scrubbers like the Warrior 510B deliver immediate drying capabilities so dining service resumes without disruption.
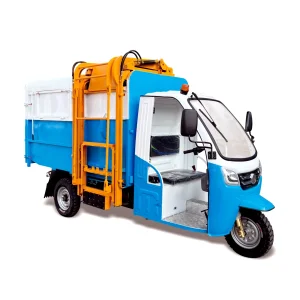
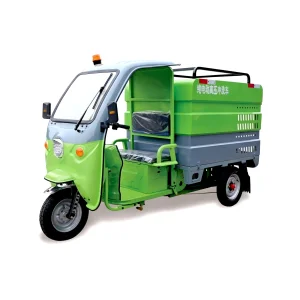
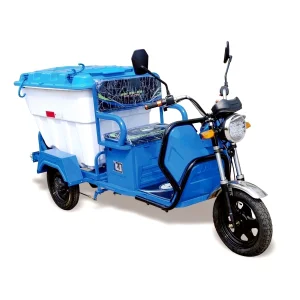
High-volume refuse transfer routes and external grease trap bays require mobile utility platforms like the LB3GT001 Dump Barrel Removal Vehicle and LB3CX600 High-Pressure Washers to break down compacted organics, dump heavy waste, and maintain municipal sanitation standards.
The future of commercial kitchen floor maintenance merges aerodynamic airflow management, intelligent battery management systems (BMS), and autonomous sensory arrays.
| Architecture Stage | Core System Engineering | Operational Functionality | Food Service Benefit |
|---|---|---|---|
| Phase 1: Present Core | Pulse Reverse Blow Filtration | High-pressure counter-burst air clearing for HEPA stages (DK-221MFC standard). | Prevents filter blinding from airborne flour and oil mist; zero downtime for manual unclogging. |
| Phase 2: Hybrid Fluidics | Oil-Aqueous Fraction Separation | Integrated coalescing plates within dual-tank chambers (DK-221VAC series). | Separates grease scum from recovered scrub water, preventing drain blockages and municipal fines. |
| Phase 3: Smart Power | LiFePO4 Modular Architecture | Automotive-grade 24V/48V lithium iron phosphate cells with CAN-bus thermal monitoring. | Rapid opportunity charging during shift changes; zero toxic outgassing around food prep zones. |
| Phase 4: Autonomous Vision | LiDAR + 3D SLAM Navigation | Multi-sensor edge-following navigation (Autonomous Scrubber series). | Handles unsupervised night-shift deep scrubbing across complex multi-table floor plans. |
Located in Wenzhou, China's precision manufacturing hub, DIKE (Wenzhou Dike Intelligent Environmental Protection Technology Co., Ltd.) leverages an integrated industrial cluster to deliver enterprise reliability and cost efficiency to wholesale partners worldwide.
From in-house rotational molding of chemical-resistant high-density polyethylene (HDPE) chassis to metal chassis laser fabrication and motor assembly, our factory eliminates intermediate supplier markups, delivering wholesale pricing structures for distributors.
Modular component architecture across our commercial floor scrubbers, vacuum units, and sweepers ensures high parts interchangeability. Universal squeegees, bypass vacuum motors, and heavy-duty casters lower inventory holding costs for global regional distributors.
Every commercial restaurant vacuum and auto-scrubber unit undergoes continuous 48-hour pressure endurance screening, circuit load testing, and fluid-recovery verification before container loading, maintaining an overseas defect rate of under 0.28%.
Importing cleaning machinery requires strict alignment with national electrical codes, worker safety regulations, and long-term service contracts. DIKE provides comprehensive documentation and localized market representation.
Configurable motor architecture supports single-phase 110V/220V (50/60Hz) alongside three-phase 380V/415V/480V installations. Fully certified under European CE directives, UL electrical safety standards, and RoHS environmental manufacturing standards.
To serve rapidly growing South Asian hospitality markets, our India Market Head (Mr. Harvansh Shandilya, New Delhi) coordinates local technical advisory, tender documentation, and rapid spare-parts distribution, backed by our global sales hub in China.
We maintain 99.4% on-shelf readiness for wear-and-tear parts—including suction hoses, rubber squeegee blades, brush drive motors, and float valves—dispatched via express freight within 24 hours of distributor request.
Straightforward answers for B2B procurement managers, hospitality supply distributors, and commercial cleaning contractors.
Commercial vacuums designed for general offices rely on paper or woven polyester filters that quickly saturate with vaporized cooking oils, leading to motor burnout and fire risks. Restaurant-grade extraction equipment features chemical-resistant seals, hydrophobic filtration, and mechanical bypass liquid shut-offs to safely manage emulsified fats and dirty wash water.
We offer comprehensive private-label manufacturing for orders meeting our minimal container volume thresholds. This covers custom rotational mold coloring, silk-screened client branding, localized operating manuals, custom packaging graphics, and country-specific plugs and wiring looms (such as BS, NEMA, or Schuko standards).
Walk-behind floor scrubbers (such as the Warrior 510B) are ideal for continuous mechanical scrubbing, detergent dispensation, and drying across open transit corridors, dining halls, and banquet spaces. High-suction industrial vacuums (such as the DK-221MFC) excel in spot fluid recovery, tight under-counter cleaning, oven cleaning, and deep fryer spill management.
Standard stock machine configurations ship within 7–10 working days. Customized OEM runs typically complete production within 20–30 days. We export through Ningbo and Shanghai ports under FOB, CIF, or DDP terms, providing full customs-clearing documentation packages including Certificates of Origin and CE compliance sheets.
Explore additional heavy-duty models manufactured in our Wenzhou production facilities, ready for immediate worldwide export and localized distribution.